Splitting reverse engineering and PCB manufacturing across vendors creates handoff gaps, respins and finger-pointing. One integrated partner owns the netlist-to-tested-board chain end to end — eliminating rework, shrinking lead time, and fixing accountability for the rebuild.
Where split-vendor projects actually fail
Almost nobody picks multiple vendors on purpose. It happens by default: an RE specialist recovers the design, a fab quotes the bare board, a contract manufacturer assembles it, a test house checks it. On paper each is competent. In practice, the project now has three or four seams, and seams are where hardware projects die quietly.
The pattern is predictable enough to write down. The RE house delivers Gerbers reconstructed from a physical board — functionally correct, but tuned for correctness, not for the fab's process window. The fab's DFM feedback comes back as a list of questions the RE house has already moved on to other projects. Layout gets patched. The board is fabricated. Then assembly discovers that a replacement component chosen during reconstruction has a footprint that doesn't quite match the panel, or that sourcing can't actually buy the alternate that was specified.
Each loop is "just a week or two." There are usually several. Meanwhile a machine sits unrepaired, a product launch slips, and the actual cause — a design that was never reviewed by the people building it — never appears on any invoice.
The anatomy of the leak: seven handoffs, seven delays
- Re-quoting and onboarding at every new vendor — each one needs files explained, requirements restated, contracts negotiated.
- File translation losses. Reconstructed design data re-entered into the fab's preferred format, then again into the assembler's — errors creep in at each conversion.
- DFM feedback that arrives too late. Manufacturability comments land after layout is "done," turning a five-minute design question into a two-week revision cycle.
- Sourcing disconnected from design. Alternates chosen during reverse engineering turn out to be unbuyable — or counterfeit-prone — when procurement finally looks.
- Physical logistics. Bare boards shipped from fab to assembler; assembled boards shipped to a tester; failed boards shipped somewhere for analysis.
- Finger-pointing on defects. A failure at test could be design, fab, or assembly. With three vendors, it's three investigations and zero owners.
- No schedule owner. Every vendor is on time by its own metrics; the end-to-end timeline still slips, because queue times between vendors belong to no one.
Fragmented vendors vs. one integrated team
This is the comparison we walk through with most new customers (a longer version lives on our Why CC Circuits page):
| Split across vendors | One integrated partner | |
|---|---|---|
| Number of suppliers | 3–5 separate companies | 1 engineering-led team |
| DFM feedback | After fabrication or assembly failures | At design and layout, before anything is built |
| Component sourcing | Checked against reality after the BOM is frozen | Aligned with the reconstructed BOM as it's created |
| Defect ownership | Investigation, then finger-pointing | One team traces test failure → assembly → fab → design |
| Communication | Email chains across time zones and vendors | Direct contact with the engineers doing the work |
| Schedule accountability | Each vendor optimized separately | Single owner from teardown to tested PCBA |
What an integrated workflow looks like in practice
Integration isn't a slogan; it's a data-flow property. When reverse engineering, layout, fabrication, assembly and test share one engineering organization, the project becomes a single connected chain:
- The reconstructed schematic is born DFM-aware. The engineers recovering it know exactly which processes and materials will build it, because they sit next to those processes.
- Component decisions are checked against real sourcing while the BOM is being written — not after. Alternates are chosen from parts that are genuinely orderable today.
- Layout review is a conversation, not a document loop. A controlled-impedance question gets answered by the people who will plate the board.
- Prototypes run on production processes. The validation unit isn't a special artifact — it's built the same way the production run will be, so what you validated is what you'll get.
- Test failures route to a cause, not a debate. The team that reconstructed the design, the line that built it, and the station that tested it share one roof and one project owner.
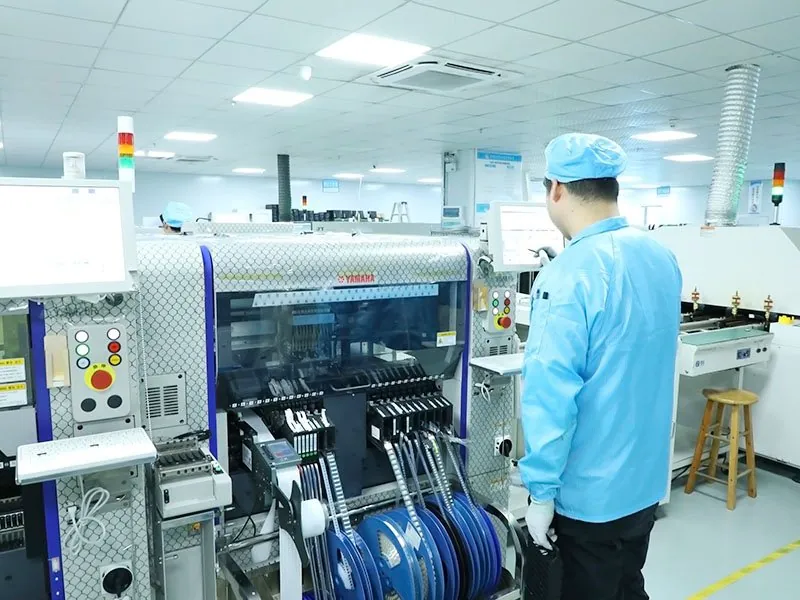
A design-for-manufacturing fix caught at the layout stage costs minutes. The same issue discovered after fabrication costs a new fab cycle; discovered after assembly, it costs fab + components + assembly; discovered at test, add debug time on top. The price of a mistake multiplies roughly tenfold at each stage it survives. Consolidation doesn't make mistakes impossible — it makes them cheap by catching them early, in one place.
Signs it's time to consolidate
- Your last two projects each needed a respin that "nobody could have predicted."
- You're spending real hours each week translating between vendors — explaining the design to the fab, the fab's questions back to the RE house.
- A defect investigation has been open for weeks with no owner.
- The board works, but every reorder requires reconstructing context from scratch.
- Your volumes are growing, and the split-vendor overhead is growing faster.
If two or three of those sound familiar, the structure — not the people — is the problem. Our approach and the full capability chain are described on the one-stop solutions page; the five-step reverse engineering walkthrough shows what the front end of that chain looks like in detail.
The takeaway
Separating reverse engineering from manufacturing doesn't look expensive on any single quote. It's expensive in aggregate: in respins that no vendor caused alone, in queues no vendor owns, in defects with no owner. One partner who designs, builds and tests what they design turns those seams into conversations in the same room.
"The cheapest respin is the one that happens at the layout review table, before anything is built."
Curious what consolidation would look like for your project? Tell us about the board — we'll scope the full chain from teardown to tested PCBA and show you where the seams are today.